Line image
INPUT · RAW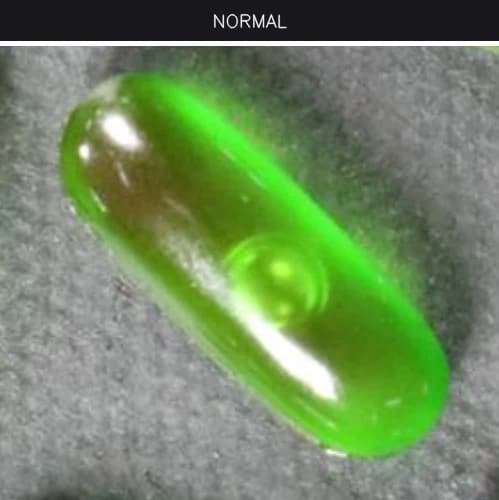
Unprocessed camera image of the gelatin capsule passing through the line.
On drug packaging, gelatin, blister, and syrup bottle lines, pill presence–absence, bottle fill ratio, and packaging defects are inspected in real time. On sterilized products, trapped air, package damage, bulging, and cap condition are checked. A light-isolated edge station installed on the conveyor compares every product with a learned perfect reference.
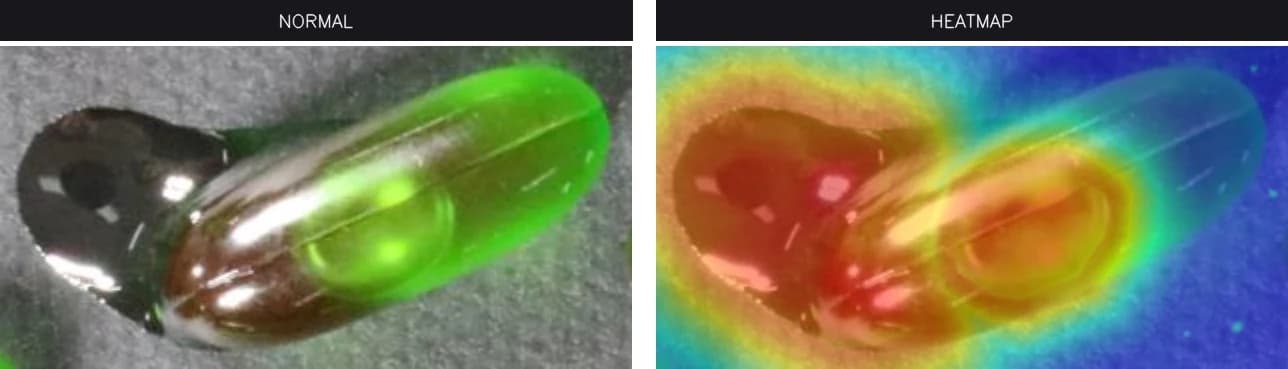 LIVE · LINE 01INSPECTION ACTIVEPACKAGING EXIT · CONVEYOR
Technical Specifications
| Installation | Light-isolated enclosed station above the packaging / filling line |
|---|---|
| Inspected products | Drug packaging · gelatin · blister · syrup bottle · sterile packaging |
| Presence – absence | Pill presence and count, cap, leaflet, and component verification |
| Fill inspection | Syrup bottle fill ratio and fill level |
| Packaging integrity | Package damage, bulging, trapped air, and cap condition |
| Packaging defects | Detection of folding, gluing, and sealing errors |
| Coding inspection | Serial number, batch code, and expiry date verification |
| Precision | Down to 6 microns depending on the optical configuration |
| Line speed | Up to 250 m/min |
| Processing | Edge / on-device — no cloud connection required |
| Anomaly threshold | Sensitivity and acceptance limit adjustable per product |
| Defect classification | Type-based labeling and reporting by defect type |
| Multiple product profiles | Profiles saved per product code; one-touch switching from the control panel |
| Positioning | By the meter via encoder; by sequence number in discrete production |
| Action outputs | Line stop · audible alert · visual alert · PLC / relay · screen · email |
| Logging & reports | Time-stamped images · daily / weekly / monthly reports |
| Visual evidence | Original image + anomaly heatmap + confidence score |
| Integration | Added to an existing packaging / filling line as an independent inspection station |
Reference · Comparison
A reference product meeting your acceptance criteria is introduced to the system first. That reference holds the fill pattern of the blister cavities, the gelatin capsule surface, the packaging surface, the cap position, and the coding area. Every product on the line is compared against this profile in real time; deviations are marked on an anomaly heatmap and converted into a numeric confidence score. The acceptance decision rests on a defined threshold, not on operator judgement.
Unprocessed camera image of the gelatin capsule passing through the line.
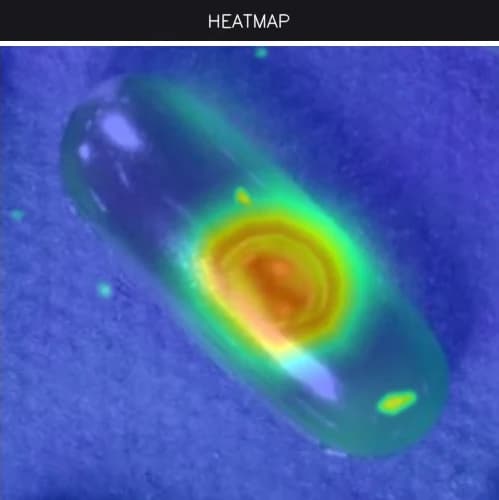
The region deviating from the reference is marked and its score checked against the acceptance threshold.
Core Capabilities
The presence and count of pills in blister cavities is verified automatically.
Syrup bottle fill ratio and fill level are measured.
Package damage, bulging, trapped air, and cap condition are checked.
Folding, gluing, and sealing errors are caught on the line.
Acceptance limit and sensitivity are defined per product; an action is produced when the threshold is exceeded.
Analysis runs on the device; no cloud connection is needed, latency stays low, and data stays on site.
With encoder integration the anomaly's position on the line is recorded by the meter, and by sequence number in discrete production.
The original image, anomaly heatmap, and confidence score are stored together.
Daily, weekly, and monthly quality reports are produced automatically.
Added to the existing line as an independent inspection station; the production flow does not change.
Anomaly Detection
Manual inspection on a production line is time-consuming, open to human error, and not sustainable. When visual quality problems are not caught early, costs grow and both product safety and brand reputation are put at risk.
Returns, rework, and loss of reputation
Quality that varies from shift to shift
Wasted labor and loss of attention
No traceability, no audit trail
Risk of a defective product reaching the field
Anomaly detection makes quality control automatic, measurable, and repeatable.
Operating Principle
In the ISEE Vision AI-powered quality control system, images are captured with industrial global shutter cameras; the analysis runs in real time on a mini NVIDIA server located on site.
The perfect pack's packaging, fill, and coding profile is saved with the product code.
Every pack is imaged under controlled lighting inside the enclosure.
Deviations are marked on an anomaly heatmap and converted into a numeric confidence score.
When the confidence score exceeds the defined threshold, an alert is raised or the line is stopped; the defect is time-stamped, logged, and reported.
The perfect product's surface, form, and dimensional profile is saved with the product code
High-speed image capture with an industrial global shutter camera
Deviations are marked on a heatmap and converted into a confidence score
Score → alert → output trigger
Display and archiving of the defective region
Alarm, stop signal, reporting
Analysis runs on the device; there is no cloud dependency
The response to each defect condition is defined in advance with a scenario specific to your site.
System Architecture
The camera system is mounted, together with industrial LED lighting, inside a sealed enclosure installed above the line. This structure protects the system from external factors, ambient light, dust, and impact. Inspection runs at the same accuracy regardless of the time of day or the shift.
Global shutter capture so a moving product's surface is imaged without motion blur
A mini NVIDIA server; instant analysis and logging matched to the line's throughput
Stable, repeatable imaging independent of ambient light
A sealed mechanical structure built for industrial site conditions
Industrial LED lighting synchronized with the camera
Added as an inspection station without modifying the existing line
Above a conveyor, on an extrusion line, or in a fixed inspection cell
Visual logging, archiving, and process tracking of defective regions
Different products previously taught to the system can also be inspected inside the same enclosure.
Technical Performance
6 µm
Surface defect detection down to 6 microns with a suitable optical configuration
250 m/min
Continuous inspection on production lines with no slowdown
360°
Full surface unwrapping with a multi-camera installation
100%
Not sampling; every product manufactured is checked one by one
Installation flexibility Conveyor, extrusion line, or fixed inspection cell
Edge processing Analysis runs on the device; no cloud connection required
Multiple product profiles Unlimited product definitions on a single station
Final values are engineered around your product, line speed, acceptance criteria, and site conditions.
Scope
The model can be customized to detect many of the defect types encountered across different sectors and production lines. Training is carried out per product and per scenario.
Scratches, cracks, blisters, tears, dents, stains, porosity
Missing hole, screw, cap, gasket, label, or component
Length, width, diameter, angle, and thickness outside tolerance
Wrong assembly orientation, reversed part, axis and alignment drift
Deformation, bending, warping, and geometric deviations
Fill level, seal integrity, and void checks
Color deviation, paint runs, print drift, tone difference
Unwanted objects inside or on the surface of the product
In short: any fault that falls outside the defined standard can be seen.
From the Field · Detections
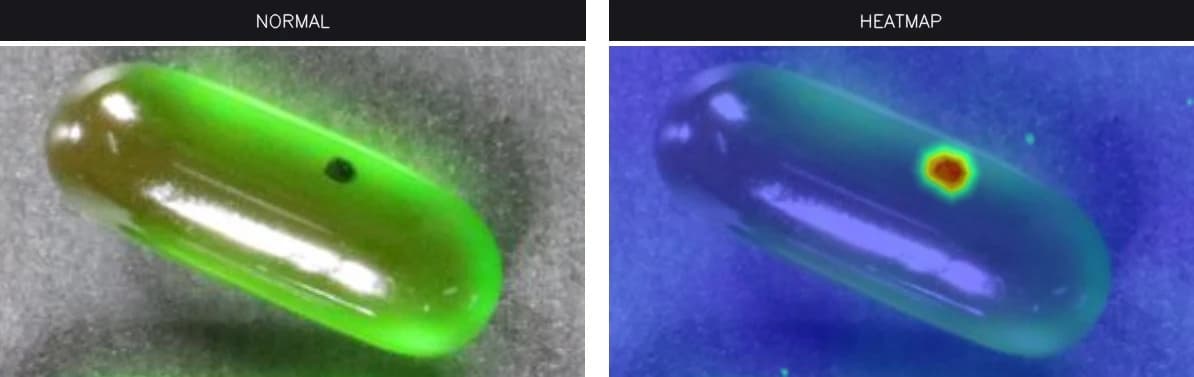
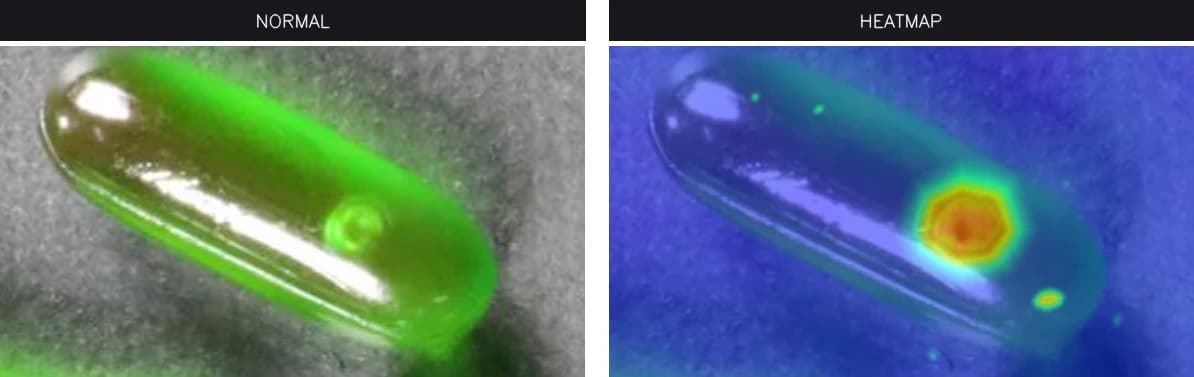
The examples below are anomaly heatmaps produced by the system in operation.
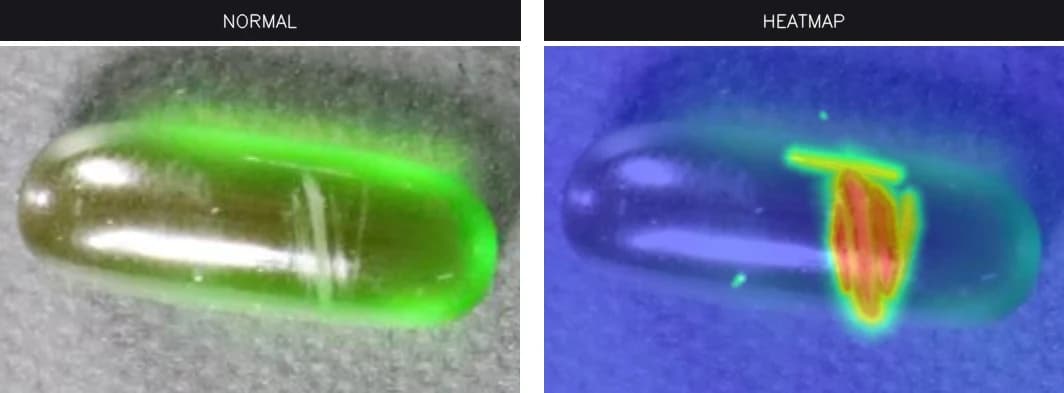
ORIGINAL + HEATMAP
Capsule crack — linear loss of continuity on the gelatin surface.
ORIGINAL + HEATMAP
Foreign matter — local dark particle on the gelatin surface.
ORIGINAL + HEATMAP
Surface bubble — local volume deviation on the capsule.
Detected Anomalies
Presence, integrity, and coding are all inspected in the same pass, against the same reference.
Missing pill, cap, leaflet, or packaging component.
Package damage, bulging, trapped air, folding and gluing errors.
Fill ratio deviation and missing or unreadable serial, batch, and date information.
Real-Time Response
The system does more than detect; it communicates directly with the equipment and teams on site to produce a response. All of these outputs can be provided individually or together.
The line is stopped automatically on a defective product through relay / PLC integration.
The operator is notified with a siren or alarm the moment an anomaly occurs.
A lamp or tower light produces a visual warning on site.
An instant notification and the defect image are shown on the operator screen.
An instant notification with images is sent to the responsible staff.
An output that connects directly to existing automation infrastructure.
Outputs can be enabled individually or together, according to what the site needs.
Traceability
Every anomaly detected is more than an instant alert: it is written into the system as a permanent, queryable quality record.
The encoder records the meter of the line at which the anomaly occurred; in discrete production, the sequence number of the part
The original image, anomaly heatmap, and confidence score are stored together
Daily, weekly, and monthly quality reports are produced automatically
Distribution analysis by defect type, product code, and shift
Detection images are archived and added to reports on request
Accumulated data is used for root-cause analysis and line optimization
The resulting data is used for traceability and process improvement in quality control.
Installation
Whether the product passes along a line such as a conveyor or an extrusion machine, or is checked inside a fixed cell, the accuracy of the inspection does not change.
Products are inspected while moving along the line. The station is positioned at the press exit, after assembly, or before packaging. On a defective product it produces a line stop and a sorting signal.
Continuously manufactured products such as cable, pipe, profile, board, and fabric receive uninterrupted surface inspection by the meter. The encoder records the defect's position along the line.
Where the product is brought to the station, full single- or multi-angle inspection is carried out inside a sealed cell. Suitable for sample checks and final quality verification.
The system is added as an independent inspection station without changing your existing production flow.
Operation
Products previously taught to the system can also be inspected inside the same enclosure. It is enough to select from the control panel which product or product number should be inspected at that moment. Changing products requires no mechanical adjustment or reinstallation.
Every product is stored with its own reference and threshold values
The operator selects the product on the panel and inspection takes effect immediately
Sensitivity and tolerance are defined separately for each product
New products are added to the system on site using a perfect sample
Quality history is reported by product code and shift
One station, unlimited product profiles: a product changeover carries no reinstallation cost.
Line Integration
The enclosure is placed over the existing packaging / filling line; the production flow does not change.
Different products are saved by product code and recalled quickly from the control panel.
Stable, repeatable images are captured independently of ambient light.
PLC / relay outputs and sorting signals connect to existing infrastructure.
Project Process
Every line is unique. The system is not applied as a standard product but engineered for your product, your line speed, and your acceptance criteria.
Product, line speed, acceptance criteria, and existing automation infrastructure are examined on site.
The camera, lens, lighting, and enclosure configuration suited to the product are determined.
Perfect product samples are taught on site and threshold values are calibrated.
PLC, relay, alert, and reporting outputs are connected to existing infrastructure.
Operator training is delivered and the model keeps improving with production data.
Share your product, line speed, and acceptance criteria; we determine the right setup for your site together.
Why Çözüm Makina
Every system we offer grows out of real problems on the factory floor. Çözüm Makina delivers not only technology but applicability and sustainability. Hardware, software, and algorithm are designed as one and applied to the site together.
Conveyor, extrusion line, or fixed inspection cell — whatever shape your production flow takes, inspection runs at the same accuracy. Surface defects, presence–absence, dimension, angle, shape, fill level, and color: every deviation beyond the defined acceptance criterion is detected, logged, and reported.
Package integrity is verified on every product against the same criterion, in a documentable way.
Configured for your line
Share your product, line speed, and acceptance criteria; we'll determine the right installation, thresholds, and action scenario together.
Related sector solutions