Line image
INPUT · RAW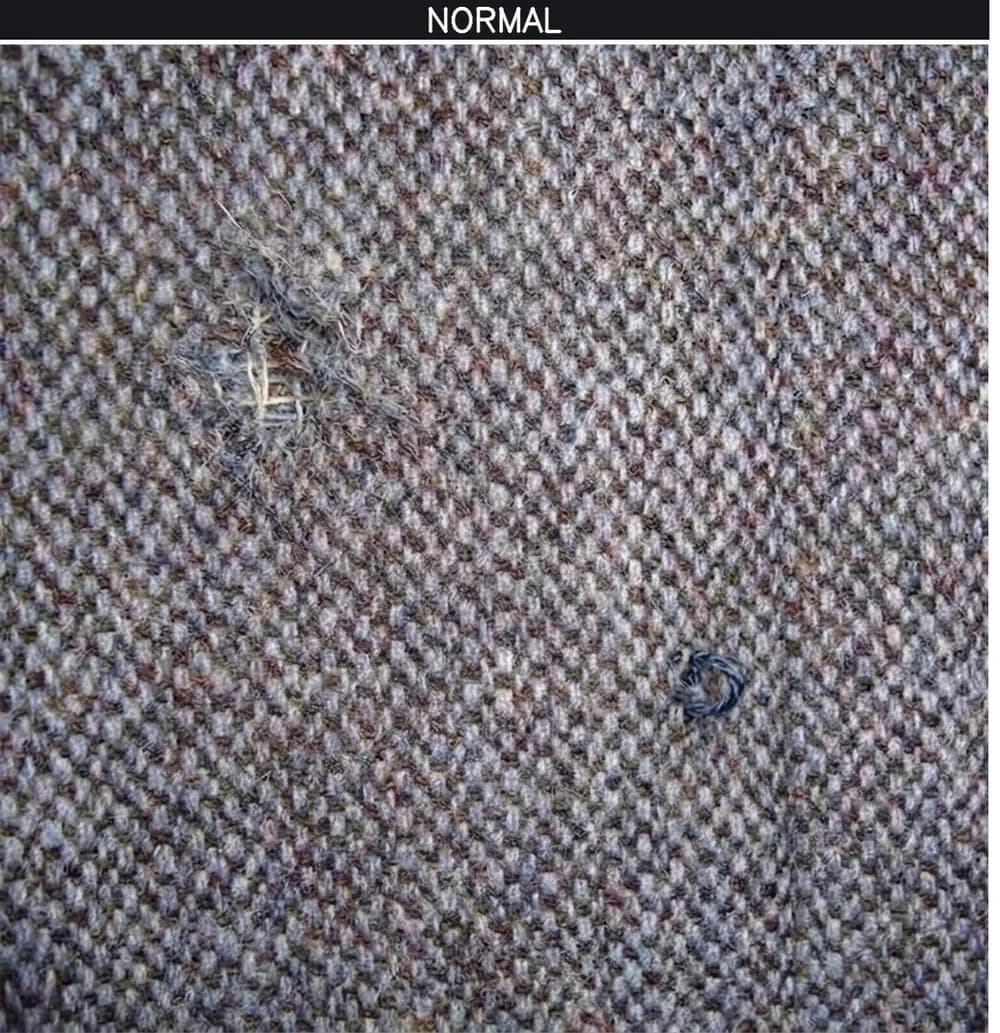
Unprocessed camera image of the panel passing through the line.
A light-isolated edge station installed on the panel and assembly line compares every part with a learned perfect reference in real time. It catches surface scratches, stains, edge-band misalignment, and missing fasteners, then stops the line or alerts the operator.
 LIVE · LINE 01INSPECTION ACTIVEPANEL EXIT · CONVEYOR
Technical Specifications
| Installation | Light-isolated enclosed station above the conveyor |
|---|---|
| Inspection method | Real-time comparison against a perfect reference panel |
| Processing | Edge / on-device — no cloud dependency |
| Surface types | Melamine / lacquered panel · upholstery fabric · woven cane · acoustic panel |
| Detected defects | Scratches, dents, stains, coating blisters, edge-band overrun, delamination |
| Presence – absence | Verification of holes, grooves, dowels, cam fittings, and fasteners |
| Color and pattern | Tone difference, pattern direction, and texture deviation checks |
| Anomaly threshold | Customer-adjustable sensitivity and acceptance limit |
| Defect classification | Type-based labels (scratch / stain / edge band / missing part, etc.) |
| Multiple products | Profiles saved per product code, switched from the panel in one touch |
| Action outputs | Line stop · siren / light · PLC / relay · operator notification |
| Logging & reports | Time-stamped images · daily / weekly / monthly reports |
| Visual evidence | Original image + anomaly heatmap + confidence score |
| Integration | Added to an existing panel / assembly line as an independent station |
Reference · Comparison
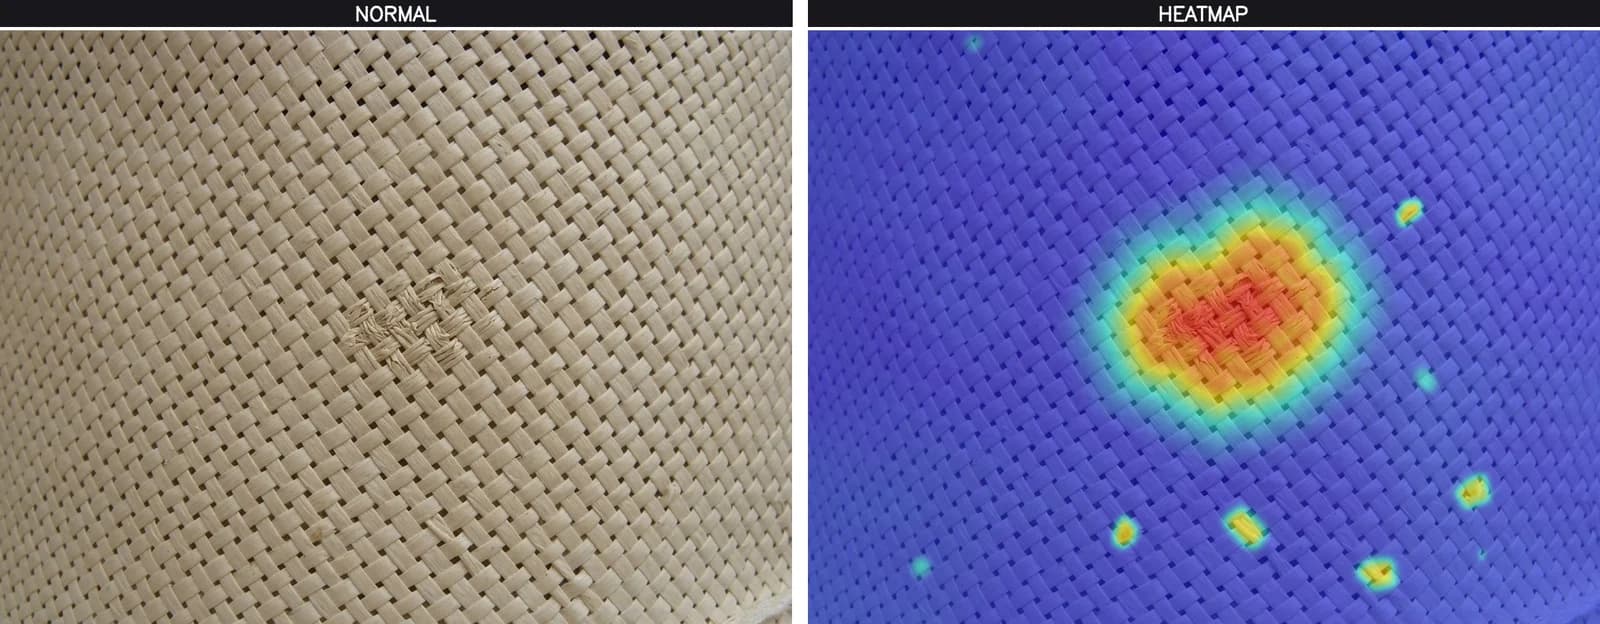
A reference panel meeting your acceptance criteria is introduced to the system first. That reference holds the surface texture, color tone, edge-band line, and hole pattern. Every panel on the line is compared against this profile; deviations are marked on an anomaly map and converted into a numeric confidence score. Surface quality moves out of personal judgement and onto a measurable criterion.
Unprocessed camera image of the panel passing through the line.
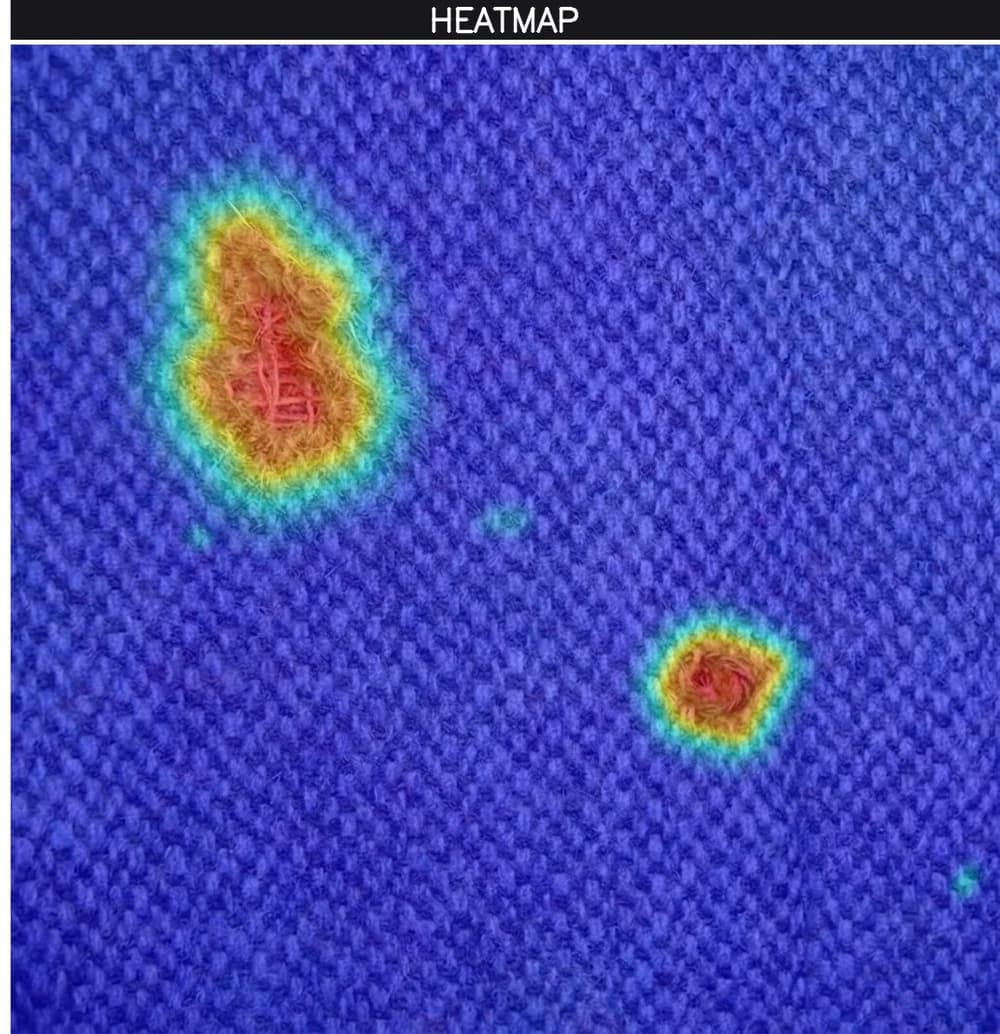
The region deviating from the reference is marked and its score checked against the acceptance threshold.
Core Capabilities
A perfect panel is learned and every deviation is measured against it.
Light isolation provides stable, repeatable imaging.
On-device analysis preserves low latency and data privacy.
Band continuity, overrun, and drift are tracked without gaps along the surface.
Holes, grooves, and fasteners are verified before assembly.
Sensitivity and acceptance limits are configured per product.
Tone difference, pattern direction, and texture deviation are compared across batches.
The source image, heatmap, and confidence score are stored together.
Added to the line as an independent inspection station.
How It Works
The perfect panel's surface, color, and hole profile is saved with the product code.
Every panel is imaged under controlled lighting inside the enclosure.
Deviations are mapped and converted into a confidence score.
When the threshold is exceeded, the system alerts or stops and records the defect.
From the Field · Detections
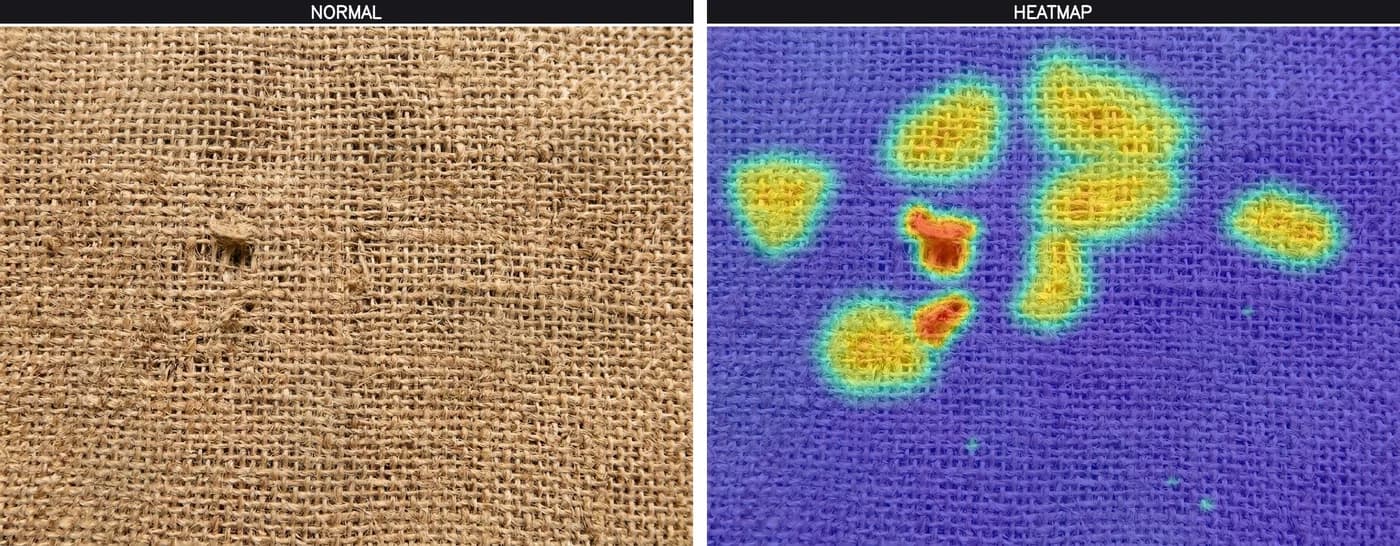
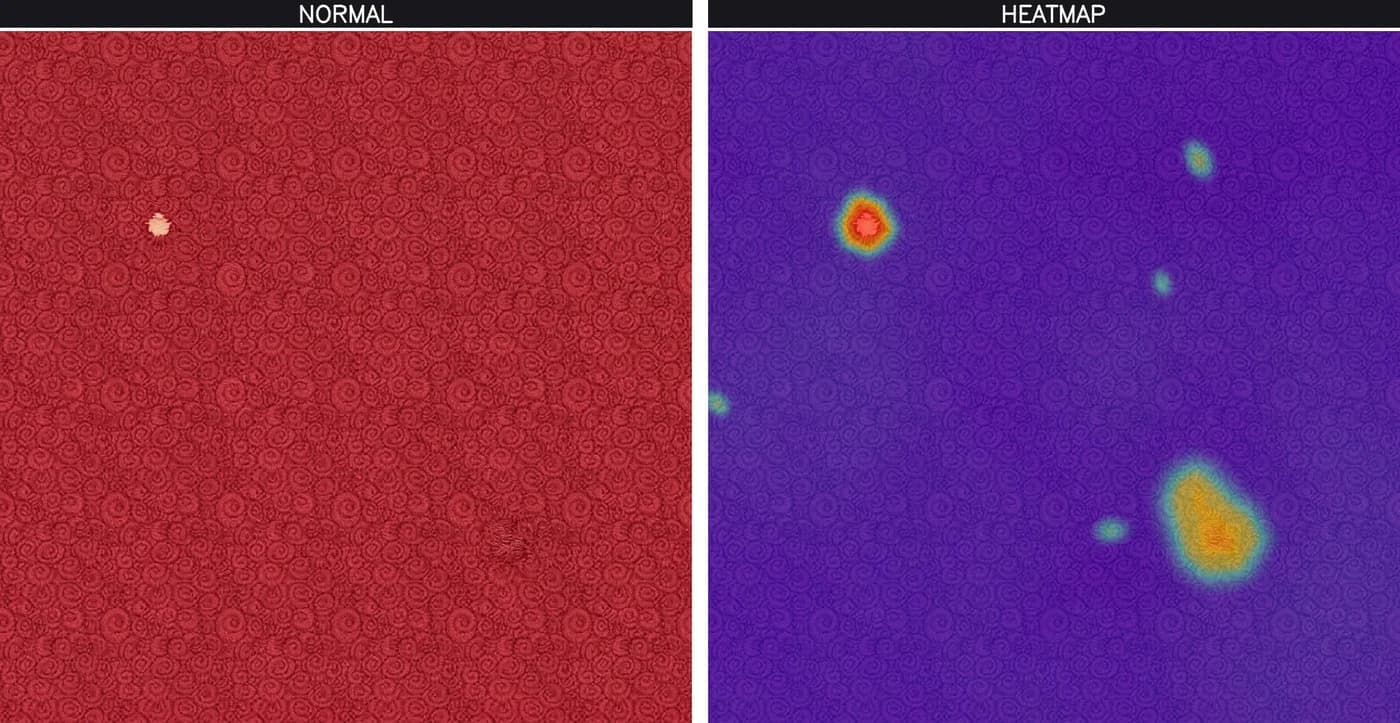
The examples below show anomaly heatmaps produced by the system.
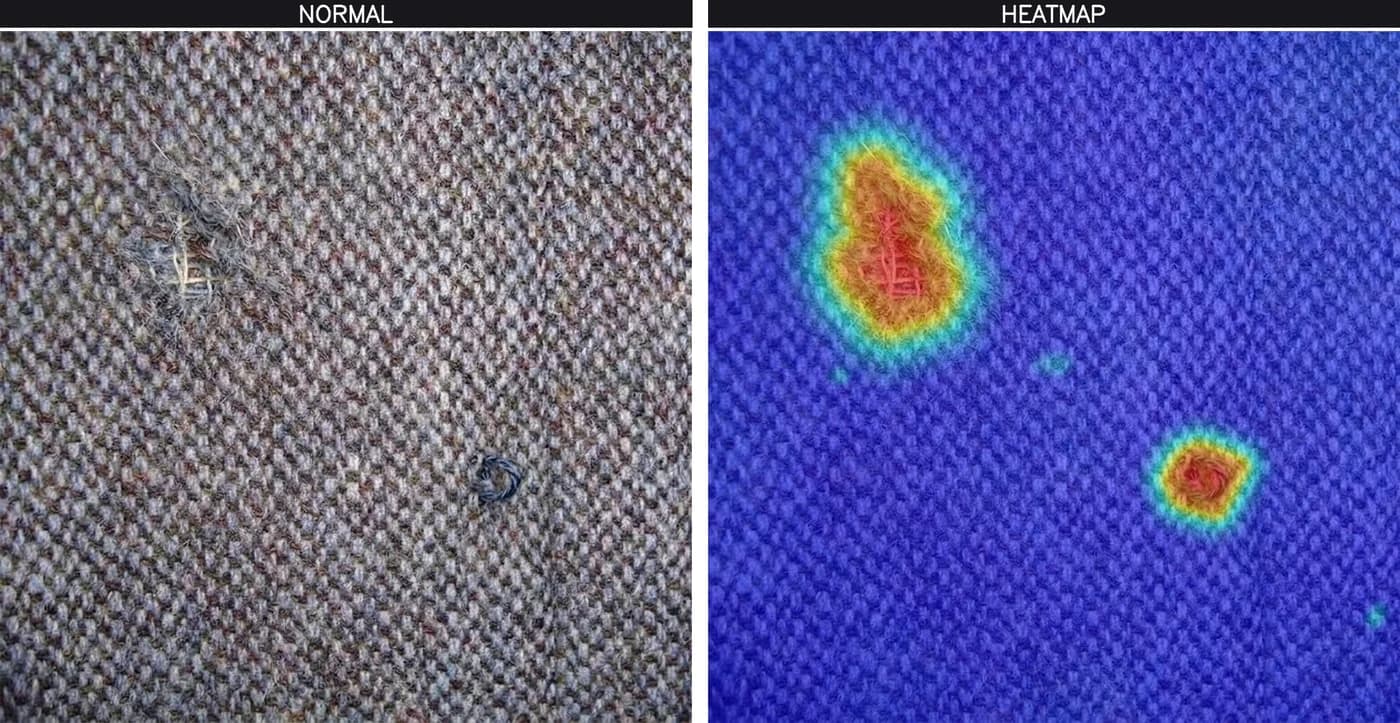
ORIGINAL + HEATMAP
Tear in upholstery fabric — loss of continuity in the weave.
ORIGINAL + HEATMAP
Hole in woven cane — local loss of texture on the surface.
ORIGINAL + HEATMAP
Surface stain — local color deviation against the reference batch.
Detected Anomalies
Surface, edge, and assembly integrity are all inspected in the same pass, against the same reference.
Scratches, dents, stains, coating blisters, and delamination; deviations that spoil the visible surface.
Edge-band overrun, drift, detachment, and loss of continuity at corner transitions.
Missing holes, grooves, dowels, and fasteners, plus incorrect positioning.
Action Outputs
Alert only, alert plus stop, or full automation—the system is configured for your production scenario.
Automatically stops the line through relay / PLC integration.
Immediately warns the operator with a siren or alarm.
Signals with a lamp or tower light.
Shows the alert and defect image on screen.
Provides outputs compatible with existing automation.
Time-stamps detections and includes them in periodic reports.
Line Integration
The enclosure is positioned directly above the conveyor.
Panels are saved by product code and recalled quickly.
Stable images are captured independently of ambient light.
PLC and relay outputs connect to existing infrastructure.
Any product that travels along a conveyor or extrusion line, or is checked in a fixed cell, can be inspected. Defects, presence–absence, dimension, angle, shape, fill level, and surface — in short, every deviation beyond the defined standard is detected.
Configured for your line
Tell us about your panel, line speed, and acceptance criteria. We'll propose the right installation, thresholds, and action scenario.